Emerson Selected to Automate Europe’s First Greenfield Sustainable Aviation Fuel Facility
Time:2026-09-30 Browse: 0
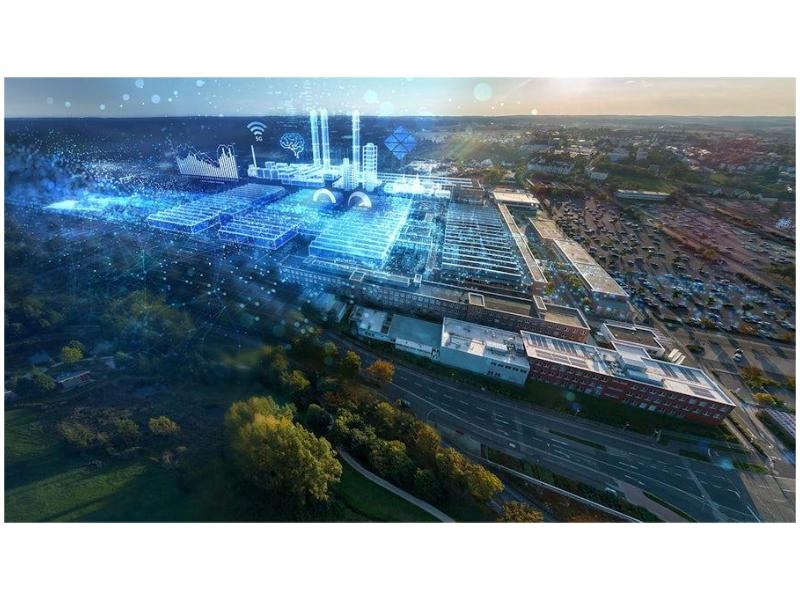
Emerson has been selected to provide automation technology for the SkyNRG sustainable aviation fuel facility currently under construction in Delfzijl, the Netherlands. Announced on September 15, 2026, the project will use an Emerson DeltaV integrated control and safety system, including DeltaV Distributed Control System and DeltaV Safety Instrumented System technologies. The facility is expected to begin operations in 2028 and is designed to produce approximately 100,000 tonnes of sustainable aviation fuel annually.
For industrial automation professionals, the project is particularly interesting because it combines process control, safety instrumentation, asset management and modular plant integration in a new greenfield facility.
Rather than upgrading an existing control system, the plant is being designed with digital automation from the beginning.
A New Greenfield Plant Designed Around Digital Automation
Greenfield projects provide a unique opportunity for automation engineers.
In an existing plant, automation upgrades often have to work around legacy equipment, old wiring, existing PLCs, older DCS architectures and previously installed instrumentation.
A greenfield project does not have the same constraints.
Engineers can design the control architecture before the physical plant is completed.
For the SkyNRG facility, Emerson's automation scope includes an integrated control and safety system intended to support process control, safety shutdown and fire-and-gas detection. The system will also use asset-management technology for commissioning and maintenance.
The project therefore provides an example of how modern industrial automation architecture can be designed as an integrated system rather than assembled from independent layers after construction.
DeltaV DCS Will Handle Process Control
The DeltaV Distributed Control System will be used to control the process units within the facility.
A DCS is particularly suitable for complex continuous and batch-related process environments because it can coordinate large numbers of process variables and control loops.
The SAF facility will contain multiple process areas, including a hydroprocessed esters and fatty acids process, a feedstock pre-treatment unit and an on-site hydrogen plant.
These processes involve different equipment and operating conditions but must operate together as one production system.
A DCS provides the central control environment for this type of process.
Typical process-control functions may include:
Temperature control
Pressure control
Flow control
Level control
Valve positioning
Pump control
Sequence management
Alarm management
Process monitoring
Operator visualization
The actual process configuration is engineered according to the plant design and operating requirements.
The important point is that the automation architecture must coordinate all of these functions while maintaining stable and safe plant operation.
Safety Instrumented Systems Add a Separate Protection Layer
The project will also use a DeltaV Safety Instrumented System.
This distinction is important for engineers working with PLC, DCS and safety automation.
A normal control system is designed to maintain the process within its operating range.
A safety instrumented system has a different role.
It is designed to respond to defined hazardous conditions and initiate predetermined protective actions.
A simplified architecture can be viewed as:
Basic Process Control System → Normal Operation
Safety Instrumented System → Independent Protective Action
Fire & Gas System → Detection and Protective Response
The exact architecture depends on the plant's hazard analysis and safety design.
For a facility producing sustainable aviation fuel, integrating process control and safety functions requires careful engineering because the plant contains chemical processing operations, hydrogen production and high-energy equipment.
The objective is not simply to automate production.
The automation system must also support safe startup, operation and shutdown.
Asset Management Becomes Part of Commissioning
Another important component of the project is Emerson AMS Device Manager.
Asset management software can provide engineers with information from intelligent field devices.
This can include device status, diagnostics and configuration information.
That becomes valuable during commissioning.
Imagine a plant containing hundreds of pressure, temperature, flow and analytical instruments.
A conventional commissioning process may require engineers to inspect individual instruments manually.
Digital device diagnostics can provide additional information that helps engineers identify configuration or device problems earlier.
This creates a connection between instrumentation and maintenance.
Instead of treating a transmitter as simply an input to the DCS, engineers can also use information from the device itself to understand its health and operating condition.
Electronic Marshalling Can Simplify Greenfield Automation Projects
The project will also use DeltaV Electronic Marshalling with distributed CHARMs.
Electronic marshalling is particularly interesting from an automation engineering perspective because it changes how field wiring and I/O configuration are handled.
Traditional control-system architecture often requires considerable planning around cabinet layouts and I/O assignments.
When field devices are connected to specific I/O cards, late engineering changes can create additional wiring and configuration work.
A more flexible I/O architecture can reduce some of these constraints.
Distributed CHARMs allow field signals to be connected through a more flexible I/O structure, supporting changes during project development.
This is particularly relevant to first-of-a-kind greenfield facilities.
Large engineering projects rarely remain completely unchanged from the first design package to final commissioning.
Process requirements may change.
Equipment vendors may change.
Instrument selections may change.
I/O counts may change.
Construction schedules may change.
An automation architecture with greater flexibility can make these changes easier to manage.
SAF Production Creates New Automation Requirements
Sustainable aviation fuel production is part of a broader industrial transition toward alternative feedstocks and lower-carbon energy systems.
From an automation perspective, new process technologies often create new control challenges.
Engineers must control:
Feedstock quality
Reaction conditions
Temperature
Pressure
Hydrogen supply
Material flow
Product quality
Energy consumption
Equipment condition
The control system must maintain these variables within their required operating ranges.
This is where process instrumentation becomes fundamental.
Sensors provide the raw information.
Transmitters convert physical measurements into usable signals.
I/O systems collect the signals.
The DCS processes the information.
Control algorithms calculate the required response.
Valves, pumps and other final control elements act on the process.
The resulting process condition is measured again.
This creates the closed-loop control structure that allows the plant to operate continuously.
Hydrogen Production Adds Another Automation Layer
The SkyNRG project will also include an on-site hydrogen plant based on a steam methane reforming technology.
Hydrogen systems require careful control of temperature, pressure, gas flows and other process variables.
The automation system therefore needs to coordinate the hydrogen production process with the broader SAF manufacturing process.
This is a good example of why modern industrial plants cannot be viewed as collections of independent machines.
The individual process units have their own control requirements, but the overall facility must operate as an integrated system.
The DCS provides the central platform for coordinating these process units.
Digital Commissioning Can Reduce Project Risk
One of the major challenges in a greenfield automation project is commissioning.
Commissioning occurs when engineering design becomes physical operation.
Problems that were invisible on engineering drawings can appear immediately:
Incorrect wiring
Wrong instrument ranges
Valve direction problems
Incorrect I/O assignments
Communication failures
Incorrect alarm settings
Control-loop instability
Device configuration errors
The earlier these problems are identified, the easier they are to correct.
That is why modern automation projects increasingly emphasize digital engineering, system staging and device-level diagnostics.
Emerson states that the integrated automation architecture for the SkyNRG project is intended to simplify commissioning and reduce project risk, including through the use of Electronic Marshalling and distributed CHARMs.
Why This Project Matters to DCS Engineers
For DCS engineers, the SkyNRG project demonstrates several trends occurring simultaneously.
First, new energy projects are becoming important users of process automation.
Second, control and safety systems are increasingly designed together from the beginning.
Third, intelligent field devices are becoming part of the plant's digital information architecture.
Fourth, flexible I/O architectures are being used to accommodate project changes.
Fifth, asset-management software is becoming increasingly connected to commissioning and maintenance.
These developments affect how automation engineers approach project design.
The engineer is no longer working only with control loops.
The complete automation environment includes:
Field Instrumentation
↓
I/O and Communication
↓
DCS
↓
Safety System
↓
Asset Management
↓
Operations and Maintenance
This integrated approach is becoming increasingly common in large process projects.
From Traditional Automation to Integrated Plant Architecture
The SkyNRG project also illustrates a larger shift in industrial automation.
Traditional automation projects were often organized around individual technologies.
The instrumentation team handled instruments.
The electrical team handled power.
The controls team handled PLC or DCS programming.
The safety team handled SIS.
The maintenance team handled equipment diagnostics.
Modern projects increasingly require these disciplines to exchange information from the beginning.
This is particularly important for first-of-a-kind facilities.
When a plant introduces a new production process, engineers cannot always rely on existing operating experience.
The control architecture therefore needs strong monitoring, diagnostics and operational visibility.
What the SkyNRG Project Means for Industrial Automation
The facility is expected to produce approximately 100,000 tonnes of sustainable aviation fuel per year once fully operational in 2028. The plant will convert residual fats and greases into a drop-in aviation fuel that can be blended with conventional jet fuel.
From an automation perspective, the project is notable because its control architecture is being designed alongside the plant itself.
The combination of DCS control, safety instrumentation, fire-and-gas detection, intelligent device management and flexible I/O creates an automation architecture intended to support the entire facility lifecycle.
For PLC, DCS, SCADA and instrumentation professionals, this type of project shows where process automation is heading: toward integrated systems in which control, safety, field diagnostics, engineering data and maintenance information work together rather than remaining isolated functions.
As new energy and sustainable-fuel facilities become more complex, automation will remain a fundamental part of making these plants controllable, maintainable and operationally reliable.